Bulk Medical Grade Hydroxyapatite Manufacturer & Wholesale Supplier
2026-09-18
- What Is Medical Grade Hydroxyapatite?
- Manufacturing Process: Ensuring Consistency in Bulk Production
- Technical Specifications and Quality Standards
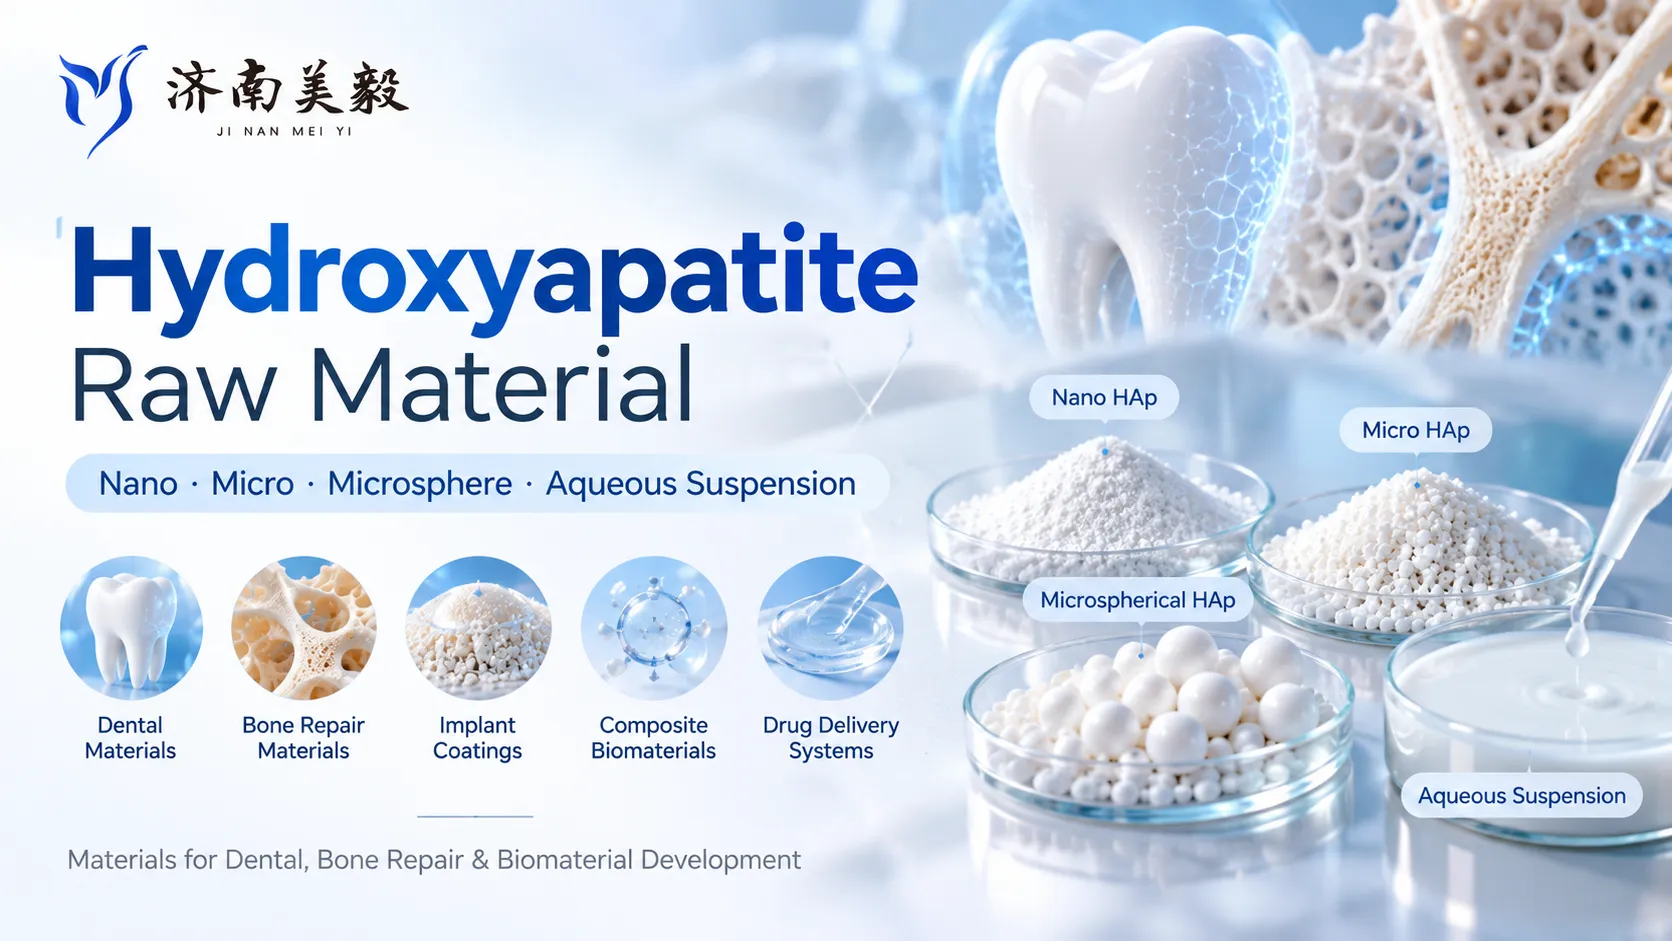
- Applications of Bulk Medical Grade Hydroxyapatite
- Hydroxyapatite vs. Other Bone Graft Materials
- How to Choose the Right Bulk Hydroxyapatite Supplier
- Common Challenges in Using Bulk Hydroxyapatite
- FAQ: Frequently Asked Questions About Medical Grade Hydroxyapatite
- Why Partner With Jinan Meiyi Biotechnology for Bulk Medical Grade Hydroxyapatite?
- Conclusion: Securing Your Supply Chain for Premium Biomaterials
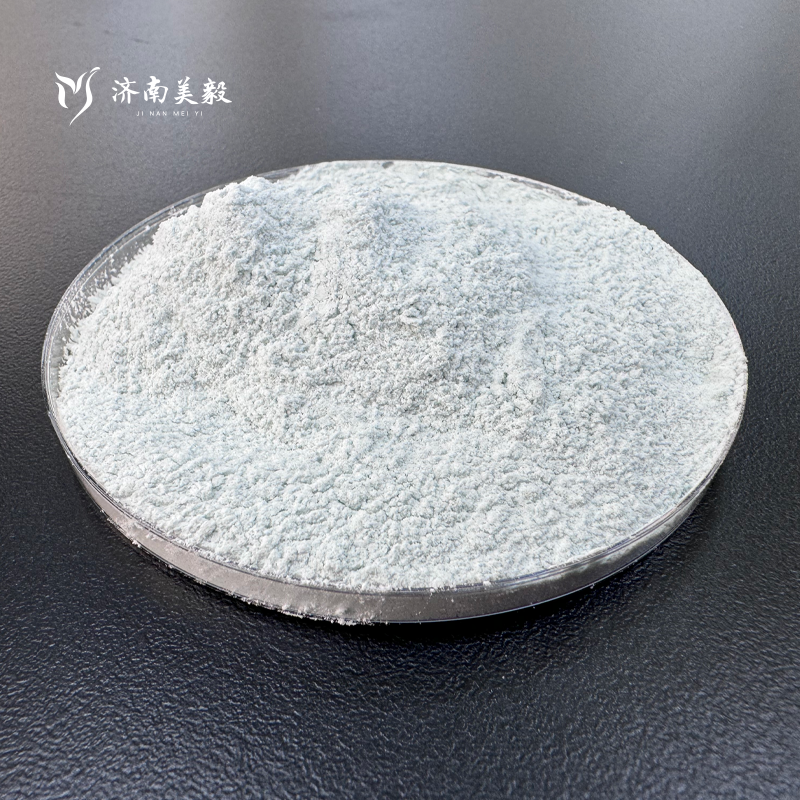
Bulk medical grade hydroxyapatite is a high-purity, biocompatible calcium phosphate ceramic widely used in orthopedic implants, dental bone grafts, and drug delivery systems. As a premier strategic sourcing partner and wholesale supplier, we provide scalable access to synthetic hydroxyapatite (HA) with precise control over crystallinity, particle size, and stoichiometry. Our materials meet stringent ISO 13485 and ASTM F1185 standards, ensuring consistent performance for regenerative medicine and biomedical engineering applications. This guide details technical specifications, manufacturing processes, and procurement strategies for sourcing premium bulk HA.
What Is Medical Grade Hydroxyapatite?
Hydroxyapatite (HA), chemically represented as Ca10(PO4)6(OH)2, is the primary mineral component of human bone and teeth. In the biomedical sector, medical grade hydroxyapatite refers to synthetically produced HA that mimics the chemical and structural properties of natural bone mineral. Unlike industrial-grade HA used in agriculture or water filtration, medical-grade variants require ultra-high purity, specific phase composition, and rigorous biological safety testing.
The value of bulk medical grade hydroxyapatite lies in its osteoconductivity. It serves as a scaffold that supports bone cell attachment, proliferation, and differentiation. When implanted, it bonds directly with host bone tissue without forming fibrous encapsulation, a process known as bioactive bonding. This makes it indispensable for load-bearing implants, coating metallic prosthetics, and filling bone defects.
Key Characteristics of High-Purity Synthetic HA
- Biocompatibility: Non-toxic, non-immunogenic, and fully resorbable or stable depending on crystallinity.
- Osteoconductivity: Promotes rapid bone ingrowth and integration.
- Chemical Stability: Resistant to physiological environments while allowing controlled ion exchange.
- Tailorable Morphology: Available as powders, granules, blocks, or porous scaffolds with adjustable pore sizes.
- High Purity: Free from heavy metals, endotoxins, and organic residues.
Manufacturing Process: Ensuring Consistency in Bulk Production
Producing bulk medical grade hydroxyapatite at scale requires advanced chemical synthesis techniques to maintain batch-to-batch consistency. Variations in pH, temperature, or reaction time can significantly alter the Ca/P ratio, crystallinity, and particle morphology, directly impacting clinical performance. The manufacturing protocols of our certified partners adhere to Good Manufacturing Practices (GMP) to ensure every kilogram meets regulatory requirements.
Wet Chemical Precipitation Method
The most common method for producing high-purity HA powder is wet chemical precipitation. This involves reacting calcium sources (such as calcium nitrate or calcium hydroxide) with phosphate sources (such as diammonium hydrogen phosphate) in an aqueous solution.
- Controlled Mixing: Reactants are added dropwise under constant stirring to prevent local supersaturation, which causes uneven particle growth.
- pH Regulation: The pH is maintained between 9 and 11 using ammonia solution. This alkaline environment favors the formation of stoichiometric HA rather than other calcium phosphate phases like tricalcium phosphate (TCP).
- Aging and Digestion: The precipitate is aged at elevated temperatures (60–90°C) to improve crystallinity and remove residual ions.
- Washing and Filtration: Multiple washing cycles remove by-products such as ammonium nitrate, ensuring high chemical purity.
Sol-Gel and Hydrothermal Synthesis
For applications requiring nano-sized particles or specific morphologies, sol-gel and hydrothermal methods are employed. Sol-gel processing offers superior homogeneity at the molecular level, resulting in highly reactive HA powders ideal for coatings. Hydrothermal synthesis allows precise control over crystal shape (e.g., rod-like vs. plate-like) by adjusting pressure and temperature conditions in a sealed vessel.
Calcination and Milling
After drying, the HA precursor undergoes calcination at temperatures ranging from 600°C to 1200°C. Lower temperatures preserve nano-crystalline structures suitable for resorbable grafts, while higher temperatures increase crystallinity for long-term stability in load-bearing implants. Post-calcination milling ensures uniform particle size distribution, critical for injectable pastes and 3D printing inks.
Technical Specifications and Quality Standards
When sourcing bulk medical grade hydroxyapatite, buyers must verify compliance with international standards. Deviations in chemical composition or physical properties can lead to implant failure or adverse biological reactions. Our products are rigorously tested against ASTM and ISO benchmarks through our comprehensive quality assurance framework.
| Parameter | Standard Requirement (ASTM F1185 / ISO 13779) | Our Typical Specification |
|---|---|---|
| Ca/P Molar Ratio | 1.67 ± 0.02 | 1.67 ± 0.01 |
| Purity | > 95% HA phase | > 98% HA phase |
| Crystallinity | Variable based on application | Adjustable (30% – 99%) |
| Particle Size (D50) | Specified by buyer | 0.5 µm – 100 µm |
| Heavy Metals (Pb, As, Cd) | < 10 ppm total | < 5 ppm total |
| Endotoxin Level | < 0.5 EU/mL | < 0.25 EU/mL |
| Sterility | Sterile or validated cleaning process | Validated cleaning, optional sterilization |
Importance of Ca/P Ratio Control
The calcium-to-phosphorus (Ca/P) molar ratio is the most critical chemical parameter. Stoichiometric HA has a Ca/P ratio of 1.67. Deviations indicate the presence of secondary phases:
- Ca/P < 1.67: Indicates calcium-deficient HA or the presence of beta-tricalcium phosphate (β-TCP). This increases resorption rate, useful for temporary scaffolds.
- Ca/P > 1.67: Suggests tetracalcium phosphate or excess calcium oxide, which can cause instability and unpredictable degradation in vivo.
Our analytical partners use Inductively Coupled Plasma Optical Emission Spectroscopy (ICP-OES) to verify elemental composition and X-Ray Diffraction (XRD) to confirm phase purity, ensuring every batch meets the exact stoichiometric requirements.
Applications of Bulk Medical Grade Hydroxyapatite
The versatility of synthetic HA allows it to be engineered into various forms for diverse medical and dental applications. Understanding these use cases helps buyers select the appropriate grade and morphology for their specific product lines.
1. Orthopedic Implants and Coatings
Metallic implants, typically made of titanium or cobalt-chromium alloys, possess high mechanical strength but lack bioactivity. Coating these metals with medical grade hydroxyapatite creates a bioactive surface that encourages bone integration. This reduces the risk of implant loosening and extends the lifespan of joint replacements (hips, knees) and spinal cages.
For bulk suppliers, this application requires HA powders with high adhesion strength and thermal stability to withstand plasma spraying processes. The coating must remain intact during insertion while promoting rapid osseointegration post-surgery.
2. Dental Bone Grafts and Periodontal Repair
In dentistry, HA is used to fill voids left by tooth extraction, periodontal disease, or trauma. It acts as a space maintainer and scaffold for new bone growth. Granular HA, often combined with collagen or autologous blood, is packed into defects to stimulate regeneration.
Dental-grade HA typically features higher porosity and specific grain sizes (0.5–2 mm) to facilitate vascularization and cell migration. The material’s slow resorption rate provides long-term volume stability, crucial for successful dental implant placement.
3. Craniofacial Reconstruction
Customizable HA blocks and cements are used in maxillofacial surgery to repair skull defects, jaw reconstruction, and facial contouring. These materials must be moldable or machinable to fit complex anatomical shapes. Injectable HA cements harden in situ, offering minimally invasive solutions for cranial repairs.
4. Drug Delivery Systems
Nano-hydroxyapatite’s high surface area and ion-exchange capacity make it an excellent carrier for therapeutic agents. It can be loaded with antibiotics, growth factors (e.g., BMP-2), or anti-cancer drugs. The HA matrix protects the drug from premature degradation and releases it in a controlled manner at the target site, enhancing treatment efficacy for bone infections or tumors.
5. 3D Printing and Additive Manufacturing
The rise of patient-specific implants has driven demand for HA-infused bio-inks and filaments. Bulk HA powder is mixed with polymers (like PCL or PLGA) to create composite materials for 3D printing. This requires extremely fine, spherical particles to ensure smooth extrusion and high-resolution print fidelity.
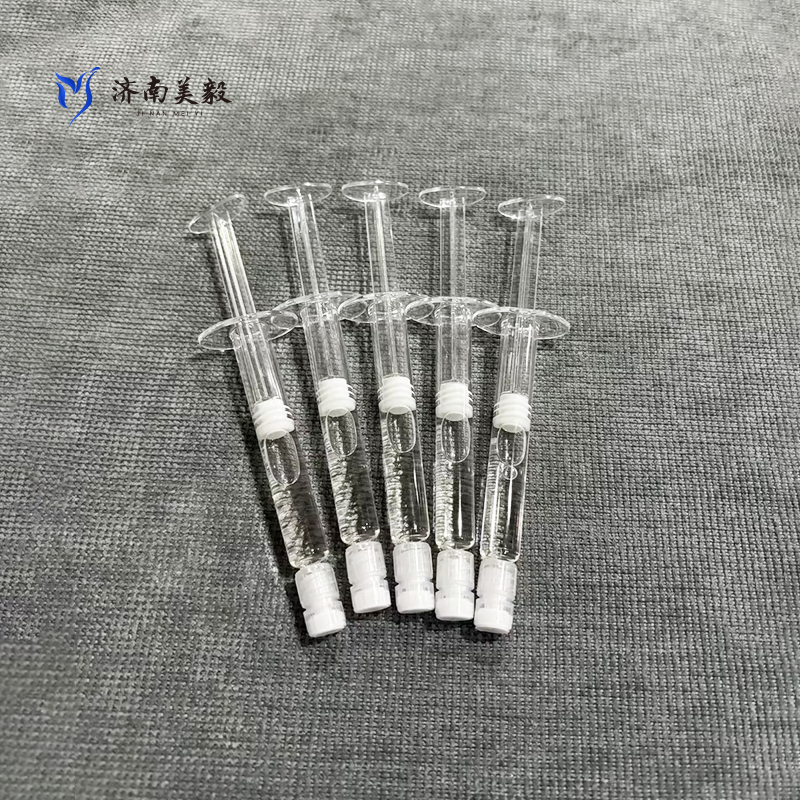
Hydroxyapatite vs. Other Bone Graft Materials
Selecting the right biomaterial depends on the clinical requirement for resorption rate, mechanical strength, and cost. Below is a comparison of medical grade hydroxyapatite with other common bone graft substitutes.
| Feature | Hydroxyapatite (HA) | Beta-Tricalcium Phosphate (β-TCP) | Bovine Bone Xenograft | Autograft (Patient’s Bone) |
|---|---|---|---|---|
| Resorption Rate | Slow (Years to Permanent) | Fast (Months) | Very Slow | N/A (Integrated) |
| Osteoconductivity | High | High | High | Highest (Osteoinductive) |
| Mechanical Strength | High (Compressive) | Low | Moderate | Variable |
| Supply Availability | Unlimited (Synthetic) | Unlimited (Synthetic) | Limited (Biological) | Limited (Surgical Site) |
| Disease Transmission Risk | None | None | Low (Processed) | None |
| Cost Efficiency | High (Bulk Scalable) | High | Moderate | High (Surgical Cost) |
Strategic Insight: Many modern formulations combine HA and β-TCP (Biphasic Calcium Phosphate, BCP) to balance stability and resorption. Through our network of certified manufacturers, we offer customized BCP ratios to optimize clinical outcomes for specific indications.
How to Choose the Right Bulk Hydroxyapatite Supplier
Sourcing bulk medical grade hydroxyapatite is a critical decision that impacts product quality, regulatory approval, and supply chain reliability. Not all suppliers adhere to the same quality standards. Here are the essential criteria for evaluating potential partners.
1. Regulatory Compliance and Certification
Ensure the supplier operates under a certified Quality Management System (QMS). Key certifications include:
- ISO 13485: Specific to medical device manufacturing, ensuring consistent design and production controls.
- ISO 9001: General quality management standard.
- REACH/RoHS Compliance: Essential for European markets, ensuring no hazardous substances are present.
- DMF (Drug Master File): For suppliers supporting pharmaceutical applications, a filed DMF indicates readiness for regulatory review.
2. Technical Support and Customization Capability
Off-the-shelf HA may not suit every application. A reputable manufacturer or distributor should offer customization services, including:
- Adjusting particle size distribution (PSD) for specific processing methods.
- Modifying crystallinity levels to control resorption rates.
- Developing composite blends with polymers or other ceramics.
- Providing detailed Certificates of Analysis (CoA) for every batch.
3. Scalability and Supply Chain Stability
For commercial medical devices, consistent supply is non-negotiable. Evaluate the supplier’s production capacity and inventory management. Can they scale from pilot batches to ton-level production without compromising quality? Do they have redundant systems to prevent supply disruptions?
4. Traceability and Documentation
Full traceability from raw materials to finished product is mandatory for medical audits. The supplier must provide comprehensive documentation, including raw material sources, processing parameters, and sterilization records. This transparency simplifies your regulatory submissions (e.g., FDA 510(k) or CE Marking).
Common Challenges in Using Bulk Hydroxyapatite
While HA is a superior biomaterial, improper handling or selection can lead to processing issues. Understanding these challenges helps engineers optimize their formulations.
Agglomeration of Nano-Powders
Nano-hydroxyapatite tends to agglomerate due to high surface energy, making uniform dispersion in polymers difficult. This can result in weak spots in composite materials. Solution: Use surface-modified HA or employ high-shear mixing and ultrasonic dispersion techniques during processing.
Brittleness of Pure HA Ceramics
Pure HA is brittle and lacks tensile strength, limiting its use in load-bearing applications alone. Solution: Combine HA with tough polymers (PEEK, PLGA) or metals to create composites that leverage HA’s bioactivity and the matrix’s mechanical strength.
Inconsistent Degradation Rates
Variations in crystallinity and porosity can lead to unpredictable resorption profiles. Solution: Specify strict crystallinity ranges and pore size distributions in procurement contracts. Request accelerated degradation data from the supplier to model in vivo performance.
FAQ: Frequently Asked Questions About Medical Grade Hydroxyapatite
Is synthetic hydroxyapatite safe for human implantation?
Yes, synthetic medical grade hydroxyapatite is biocompatible and bioactive. It is chemically identical to the mineral phase of human bone. When produced under GMP conditions and sterilized, it poses no risk of immune rejection or disease transmission, unlike some animal-derived grafts.
What is the shelf life of bulk hydroxyapatite powder?
When stored in a cool, dry environment in sealed containers, synthetic HA powder is chemically stable indefinitely. However, for medical applications, manufacturers typically assign a shelf life of 2–5 years to ensure sterility packaging integrity and prevent moisture absorption that could affect processing characteristics.
Can hydroxyapatite be sterilized?
Yes. HA is thermally stable and can be sterilized using autoclaving (steam sterilization), gamma irradiation, or ethylene oxide (EtO) gas. The chosen method depends on the final formulation. For pure powders, gamma irradiation is common. For polymer composites, EtO or low-temperature plasma methods may be preferred to avoid degrading the polymer.
What is the difference between crystalline and amorphous hydroxyapatite?
Crystalline HA is more stable and resorbs slowly, making it suitable for long-term implants and coatings. Amorphous or low-crystallinity HA is more soluble and resorbs faster, which is beneficial for temporary scaffolds where rapid bone replacement is desired. The choice depends on the required duration of scaffold support.
Do you provide custom particle sizes?
Yes, through our specialized manufacturing partners, we offer custom milling and classification services. We can produce sub-micron powders for coatings and injectables, or larger granules (1–4 mm) for bone void fillers. Particle size distribution is verified via Laser Diffraction analysis.
Why Partner With Jinan Meiyi Biotechnology for Bulk Medical Grade Hydroxyapatite?
In 2026, the demand for reliable, high-quality biomaterials continues to grow. Jinan Meiyi Biotechnology Co., Ltd., headquartered in Jinan, Shandong Province, serves as a trusted enabler for innovation across the global personal care and aesthetic medicine value chain. As a subsidiary of Pacific Kangtai Scientific Instruments (Jinan) Co., Ltd., we specialize in the research, development support, and commercialization of bioactive technologies.
Unlike traditional manufacturers, Jinan Meiyi Biotechnology operates as a strategic sourcing and quality-assured distribution partner. We do not engage in direct manufacturing; instead, we leverage a well-established global supply chain network to partner with internationally recognized, certified manufacturers. This model allows us to focus exclusively on what matters most to our clients: scientific rigor, regulatory compliance, and market responsiveness.
Our Core Competencies
- Quality-Assured Global Sourcing: We maintain long-term cooperative relationships with top-tier suppliers who adhere to ISO 13485 and other international quality management systems. Every raw material undergoes comprehensive evaluation, including efficacy data, stability profiles, and compatibility checks, before inclusion in our portfolio.
- Regulatory Intelligence & Traceability: Our quality assurance framework centers on supplier qualification, documentation traceability, and batch-level specification verification. Each shipment of bulk HA is accompanied by full technical dossiers, including Certificates of Analysis (CoA), safety data sheets, and regulatory status summaries, simplifying your FDA 510(k) or CE Marking submissions.
- Technical Partnership Model: We serve R&D laboratories, CDMOs, and aesthetic clinics with a service philosophy rooted in partnership rather than transaction. Our scientifically trained team provides technical consultation and collaborative problem-solving, helping you navigate the complexities of bioactive ingredient science.
- Reliable Logistics & Integrity: We maintain strict control over storage conditions, shipping protocols, and delivery timelines to ensure product integrity from origin to end-user. Our global logistics capabilities ensure compliant documentation for customs and regulatory clearance across Asia, Europe, and North America.
Commitment to Sustainability and Science
We actively monitor emerging trends in bioactive ingredient science and dermatological research, integrating these insights into our portfolio strategy. By partnering with manufacturers who adhere to green chemistry principles, we help minimize waste and energy consumption while maintaining the highest standards of product purity. This aligns with the growing corporate responsibility goals of medical device manufacturers globally.
Conclusion: Securing Your Supply Chain for Premium Biomaterials
Bulk medical grade hydroxyapatite is a foundational material in modern regenerative medicine. Its unique ability to integrate with human bone makes it irreplaceable in orthopedics, dentistry, and craniofacial surgery. However, the quality of the final medical device is only as good as the raw material it starts with. Sourcing from a certified, experienced partner like Jinan Meiyi Biotechnology ensures consistency, regulatory compliance, and clinical success.
Whether you are developing next-generation dental grafts, orthopedic coatings, or innovative drug delivery systems, the purity and physical properties of your HA powder are paramount. Do not compromise on quality. Partner with a supplier who understands the science, the standards, and the stakes.
Ready to optimize your production?
Contact our technical sales team today to request a sample, review our full specification sheet, or discuss custom manufacturing requirements. Let Jinan Meiyi Biotechnology support your innovation with reliable, high-performance hydroxyapatite solutions backed by scientific integrity and global expertise.
Explore Our Full Range of Bioceramic Materials and Technical Solutions



Please leave us a message.